How to use PUR hot melt adhesive correctly depends on the product grade, substrate and application equipment. Reactive PUR is applied hot and then develops its final properties as it cures with moisture. For general background on the polymer family, see polyurethane. This guide covers preparation, application, storage and cleaning so a production team can build a controlled process around the adhesive’s technical data sheet (TDS).
Nội dung bài viết
Choose equipment designed for reactive PUR
PUR hot melt needs a compatible melter, tank or cartridge system and an applicator suited to the required bead or coat. The equipment must maintain the specified temperature and limit unwanted moisture exposure. A standard craft glue gun is not a substitute for a production PUR applicator. Inspect the feed path, nozzle, seals and controls before starting work. For application context, see TECHBOND’s English PUR adhesive overview.
- Melting and feed system: Match it to the adhesive package and required output; verify stable, measured temperature.
- Applicator: Select a nozzle, roller or coating head that produces the specified glue pattern and coat weight.
- Process controls: Monitor temperature, line speed, pressure and material position so the bond is repeatable.
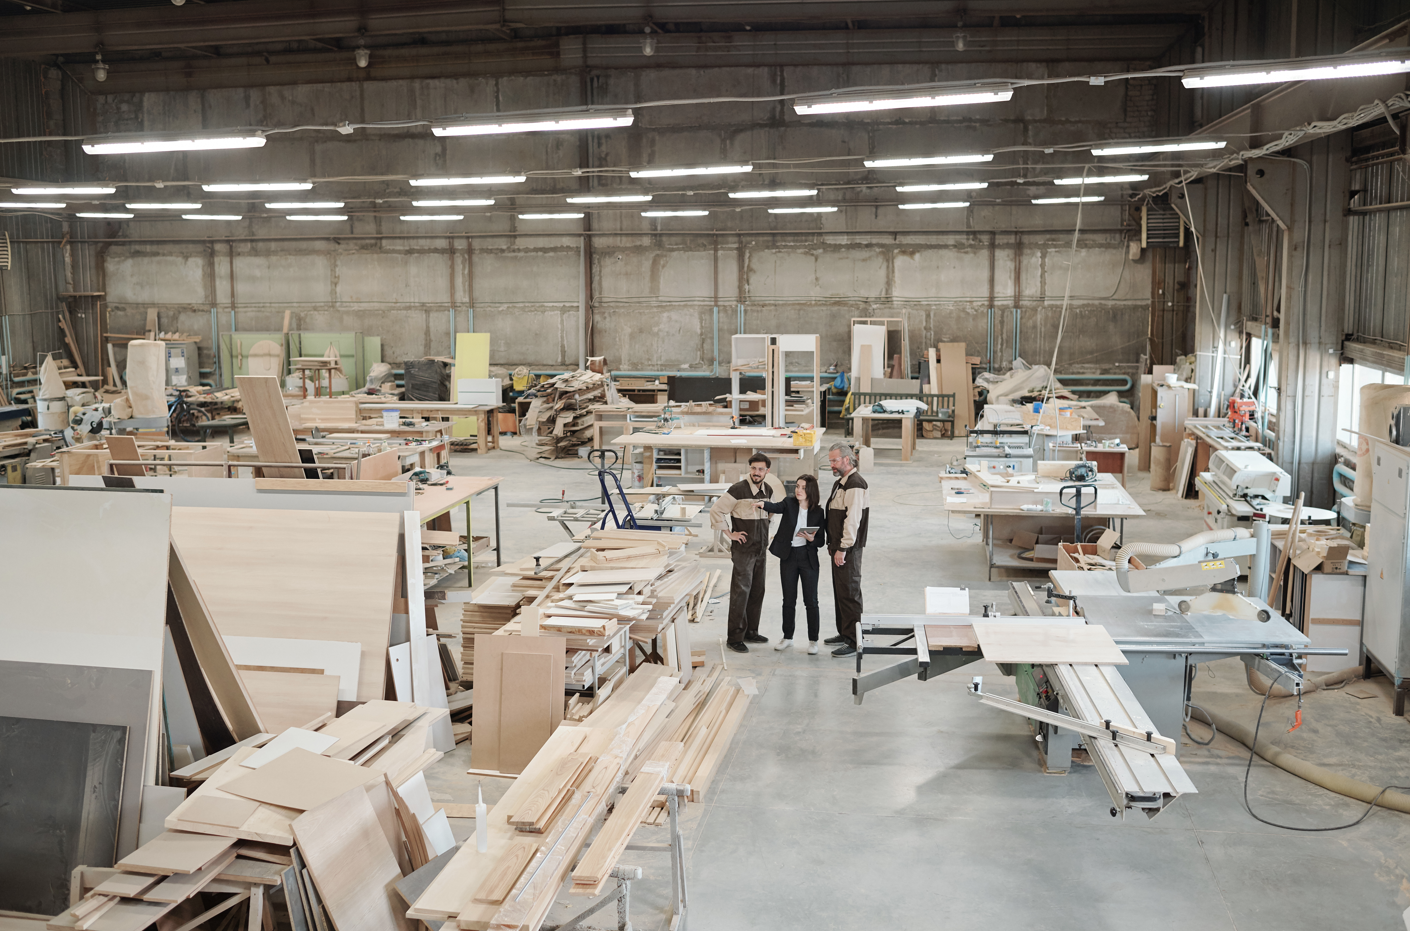
PUR application equipment and process setup.
How to use PUR hot melt adhesive: a practical sequence
1. Check and prepare the equipment
Before loading adhesive, inspect the melter, hoses, application head and temperature controls. Remove residue using the approved procedure so old cured material does not block flow. Check that seals and the system configuration limit moisture entry. Follow the machine maker’s safety and maintenance instructions when working around heated parts.
2. Prepare the substrates
Identify both materials and clean the bonding areas. Dust, oil, loose particles and excess surface moisture can reduce adhesion. Confirm that the substrate and any coating are compatible with the selected PUR grade. Run a small trial before committing to a new material combination.
3. Set the working temperature
Use the temperature range specified in the TDS for the exact grade and measure the actual temperature at the relevant points. The Vietnamese source gives a broad example of 120–180°C, but it must not be treated as a setting for every PUR product. Too much heat can damage the adhesive; too little may prevent even application.
4. Apply the adhesive evenly
Use the compatible nozzle, roller or coating head to deliver the specified amount. Too little adhesive can leave dry areas, while an excessive coat may affect appearance and cost. Check the pattern and weight on representative production samples.
5. Assemble within the open time
Bring the surfaces together within the grade’s stated open time and apply the required, uniform pressure. The source mentions a 10–60 second example; the actual window varies with formulation, coat weight, substrate and conditions. Confirm the settings through a line trial.
6. Allow the bond to cure
Initial handling strength is not the same as final performance. Moisture curing continues after assembly, and full cure time depends on the grade and environment. The source notes that some applications may take up to 24 hours. Follow the relevant TDS before testing final strength or releasing the finished product.
Important operating checks
- Limit air and moisture exposure: Keep containers and compatible equipment closed as instructed. Premature reaction can shorten usable time or create blockages.
- Keep temperature stable: Watch actual machine readings throughout the run; investigate unexpected viscosity or flow changes.
- Record ambient conditions: Temperature and humidity can affect assembly and cure. Use the approved operating window for the chosen product.
Which materials can PUR hot melt bond?
Depending on the formulation, PUR hot melt may be evaluated for wood products, decorative laminates, fabrics, leather, selected plastics, metals or films. Material names alone do not establish compatibility. For example, untreated polypropylene can be difficult to bond; surface preparation or a different grade may be needed. Test the actual substrate pair and intended service conditions. Explore TECHBOND woodworking adhesives for furniture applications.
Storage and shelf life
Store unopened PUR in its original sealed packaging under the supplier’s stated temperature and humidity conditions. Protect it from heat, sunlight and moisture. Mark opened containers and follow the specified reuse window. Inspect the material before loading: skinning, contamination or abnormal flow can indicate that it should not be used. Avoid mixing fresh and degraded adhesive without a validated procedure.
Protect PUR from moisture and follow the equipment cleaning schedule.
How to clean PUR hot melt equipment
When cleaning is needed
Clean according to the machine and adhesive supplier’s schedule, especially before changing grades, after an extended shutdown or when flow suggests contamination or cured residue. Reactive PUR can be difficult to remove after curing, so timely maintenance matters.
Cleaning procedure
- Stop production and isolate the equipment using the maker’s safety procedure.
- Use only the specified purge compound or cleaner compatible with the adhesive system and internal coatings.
- Clean the tank, feed path and application head in the sequence recommended for the equipment.
- Check that residue and cleaning material have been removed before reloading adhesive.
The source gives a general cool down instruction, but safe cleaning temperature and sequence depend on the machine and cleaner. Do not use sharp tools that can damage the applicator or nonstick surfaces.
Ask TECHBOND about your process
Knowing how to use PUR hot melt adhesive on a specific line requires the grade TDS and a trial with the actual substrates. Share your material pair, machine model, target coat weight and performance requirements with TECHBOND so our team can help plan a suitable evaluation.
TECHBOND MFG (VIETNAM) CO., LTD.
Address: No. 18, Street 23, VSIP II-A Industrial Park, Vinh Tan Ward, Tan Uyen City, Binh Duong Province, Vietnam
Sales hotline: +84 866 15 37 68
Email: info@techbond.com.vn
TECHBOND Vietnam is a leading manufacturer of industrial adhesives in Vietnam. We specialize in providing a wide range of flexibly customized adhesive products to meet the diverse requirements of our customers.
Need advice on the right industrial adhesive?
Share your materials, application and production process. TECHBOND will help recommend a suitable solution.
Request a consultation