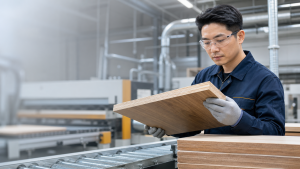
Adhesive bond failure after pressing does not automatically mean the adhesive is wrong. A weak joint can result from surface condition, material moisture, application consistency, press settings, line speed or curing. Before changing adhesive, check the process in a fixed order and compare each setting with the adhesive supplier’s technical data sheet (TDS) and your approved production window.
Nội dung bài viết
1. Contamination or poor surface preparation
Dust, oil, release agents, printing residues and loose fibres can keep adhesive from wetting the substrate. Rough, damaged or uneven surfaces can also leave gaps in the bond line. Check the material at the point of application, confirm that cleaning methods do not leave residue, and keep prepared surfaces protected from handling contamination. If failures cluster in one area, compare the surface there with a sound joint rather than assuming the adhesive batch is at fault.
2. Uneven or excessive material moisture
Moisture can change how porous materials absorb adhesive and how they respond during pressing. A wet or uneven substrate may weaken contact, slow drying or create variation from one part of a sheet or batch to another. Measure and record moisture using the method approved for the material, and compare readings across both bonded surfaces and production lots. Follow the material and adhesive specifications; do not compensate for moisture variation by changing adhesive quantity without a controlled trial.
3. Press temperature is wrong or uneven
A displayed setpoint may not reflect the temperature across the working area. Cold zones can delay activation or drying, while excessive heat may shorten open time or alter adhesive flow. Verify actual temperatures with a calibrated method at representative points, including the edges and centre, and allow the equipment to stabilise. Record the material temperature as well as the press setting where relevant. Make one approved adjustment at a time and check the result on a consistent sample.
4. Pressure or pressing time is inconsistent
Insufficient pressure may prevent close contact; uneven pressure can leave weak areas even when the average setting looks correct. Too little time may not allow the adhesive to develop the required bond, while unnecessary extra time can reduce throughput without fixing a preparation problem. If adhesive bond failure after pressing repeats in one press position, compare that area with a sound joint. Check pressure distribution, platen alignment, loading and dwell time against the adhesive TDS and machine procedure. Compare samples from different positions in the press to identify whether the defect follows a location or a material batch.
5. Adhesive amount or viscosity varies
Too little adhesive can leave gaps or incomplete coverage. Too much can squeeze out, extend drying or curing, and create an unstable bond line. Viscosity changes with temperature, storage, mixing and time in the production system, so inspect the adhesive condition and application equipment together. If adhesive bond failure after pressing occurs across batches despite steady settings, review the process record before changing the adhesive. Check coat weight or applied quantity using the plant’s normal measurement method; inspect rollers, nozzles and metering for wear or blockage. Use the supplier’s handling and preparation instructions, and avoid adding water or other materials unless the product guidance specifically permits it.
6. Line speed exceeds the process window
When line speed changes, the adhesive may have less time for open assembly, wetting, pressing or drying. A setting that works at one speed may not work at another. When adhesive bond failure after pressing begins after a speed change, compare the current speed with the approved process window and note any recent changes to shift, equipment, material or ambient conditions. Check that application and press timing remain synchronised throughout a run, not only during start-up. If a trial is needed, change speed in a controlled step and record the resulting bond performance.
7. Inadequate curing, storage or post-press handling
A joint can appear acceptable immediately after pressing and still fail if it is handled before it has developed sufficient strength. Stacking, loading, trimming or moving products too early may stress the bond. Check the required cure or conditioning time, temperature and storage conditions in the TDS, and keep adhesive containers sealed and stored as specified. Review whether failures occur after a delay or after a particular handling step; that timing can help distinguish curing or storage issues from poor initial contact.
A practical troubleshooting sequence
- Describe the failure: where it occurs, when it appears, and whether it is consistent or intermittent.
- Separate a clean adhesive-interface failure from substrate damage or material failure.
- Check substrate cleanliness, surface condition and moisture on both bonded sides.
- Verify adhesive identity, condition, application amount and equipment consistency.
- Measure actual press temperature, pressure, dwell time and line speed against the approved process window.
- Review curing, storage and post-press handling, then change one variable at a time and record the result.
Quick inspection checklist
| What to inspect | Questions to ask |
|---|---|
| Surface | Are the substrates clean, sound and consistent at the bond area? |
| Moisture | Are readings within the material and adhesive process requirements? |
| Pressing | Are temperature, pressure and dwell time verified across the working area? |
| Application | Are quantity, viscosity and coverage steady from start to finish? |
| Production and curing | Did line speed, cure time, storage or handling change? |
Frequently asked questions
Does adhesive bond failure after pressing always mean the adhesive is unsuitable?
No. Adhesive suitability is one factor, but surface preparation, moisture, application and press conditions can produce similar symptoms. Check these variables before changing products.
Which setting should I check first?
Start with the failure pattern and the bond surfaces, then verify moisture, application and actual press conditions. There is no single setting that explains every failure.
Should I increase the adhesive amount to improve bond strength?
Not without checking coverage, viscosity and the product specification. More adhesive can cause squeeze-out or slower drying and may not correct contamination or poor contact.
What information helps diagnose a recurring failure?
Record substrate type and condition, adhesive grade and batch, application amount, line speed, actual press settings, cure time, failure location and photographs of the joint. Share these details with your adhesive supplier or process team for a focused review.
Before changing adhesives, document the conditions of both a failed and a sound bond. If adhesive bond failure after pressing continues, share the substrate, adhesive, process settings and failure photos with your TECHBOND technical team for a focused discussion. Confirm product-specific limits with the current TDS and your technical team.
For broader woodworking manufacturing context, see the Woodworking Network Best Practices Guide; it does not replace product-specific technical guidance.
TECHBOND Vietnam is a leading manufacturer of industrial adhesives in Vietnam. We specialize in providing a wide range of flexibly customized adhesive products to meet the diverse requirements of our customers.
Need advice on the right industrial adhesive?
Share your materials, application and production process. TECHBOND will help recommend a suitable solution.
Request a consultation