One-component PVAc wood glue for finger jointing is a ready-to-use adhesive used to join shorter timber pieces into longer, stable components. Finger-jointed wood is common in furniture, flooring, interior finishing and other wood products. This guide covers adhesive selection, preparation and the finger-jointing process.
Nội dung bài viết
What is one-component PVAc wood glue?
One-component PVAc wood glue is a water-based adhesive based on polyvinyl acetate. It is typically milky white and can be applied directly without mixing. A single-component system can simplify handling on production lines, but the selected grade must still match the wood, machine and required bond performance.
Characteristics and adhesive selection
- Suitable grades can bond a range of wood substrates and work with common woodworking equipment.
- Drying time, viscosity and open time vary by product and process; confirm the current Technical Data Sheet (TDS).
- Some TECHBOND grades are classified D2 or D3 under relevant EN 204 test conditions. Verify the classification and intended use for the exact product.
- Ready-to-use handling removes a mixing step. It does not remove the need to control spread, assembly time, pressure and curing.
Choose an adhesive by considering wood species, moisture, storage history, surface quality, joint design, application method and production speed. Smooth, freshly machined surfaces and a correctly fitted finger profile help create consistent contact. Ask the technical team to confirm viscosity and application suitability for roller, scraper, nozzle or direct-pour systems.
Applications of PVAc adhesive in finger-jointed wood
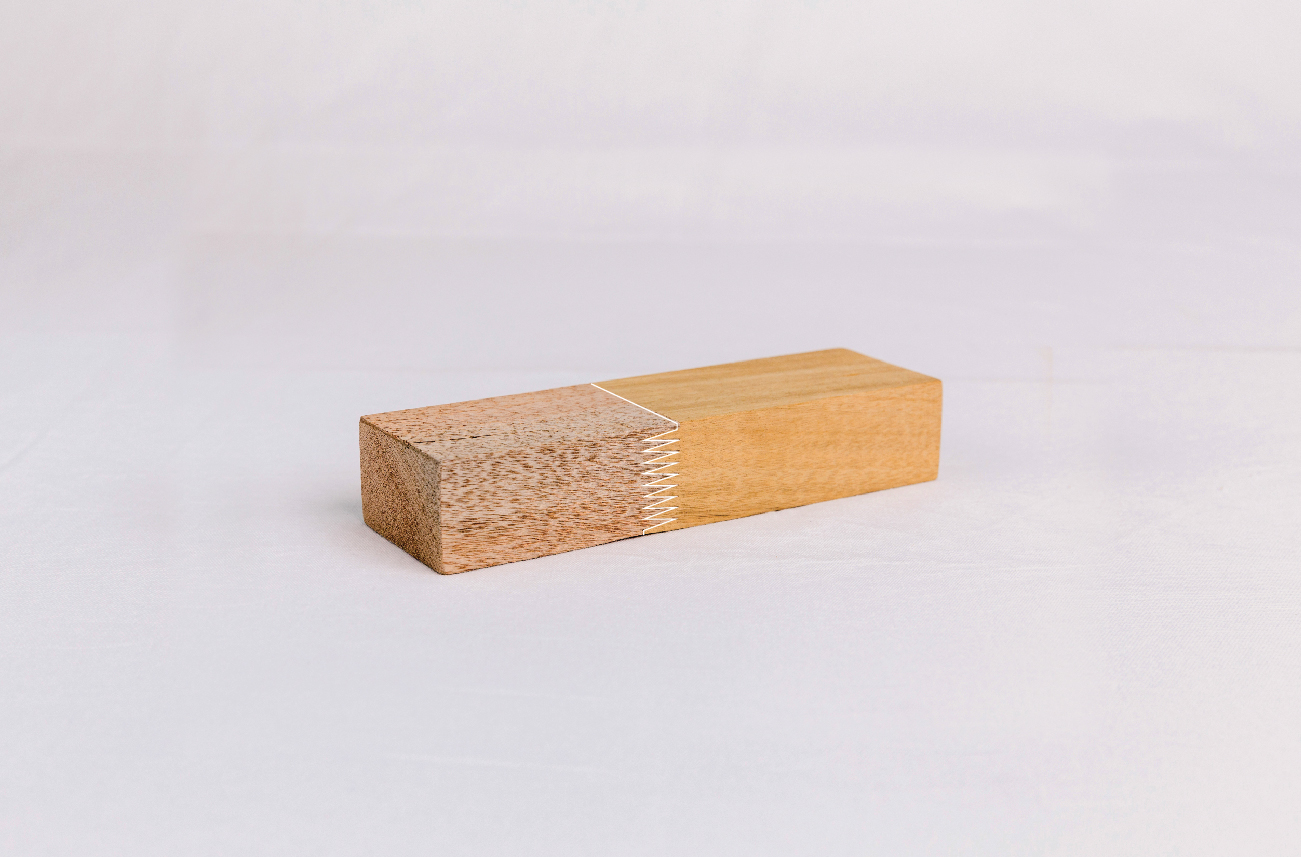
Finger-jointed wood is made by machining short pieces with interlocking tooth-like profiles and joining them into longer elements. It is used in furniture, flooring, interior components and panels. Depending on the product specification, PVAc adhesives may also be suitable for edge lamination, assembly and mortise-and-tenon joints. Paper and packaging applications require an adhesive grade designed for those substrates.
Finger jointing process with one-component PVAc wood glue
1. Prepare the wood
Keep bonding surfaces smooth, even, clean and free from dust, oil and grease. Machine finger profiles accurately so the joint closes without visible gaps. A moisture content around 8%–12% is a reference stated in the source process; confirm the acceptable range for the selected wood and adhesive with the current TDS and production trials.
2. Apply and assemble
Apply the adhesive directly without mixing. Spread it evenly across the required bonding area and use enough adhesive to achieve full contact through the finger profile. The Vietnamese source process specifies at least 50% surface coverage and assembly within 3 minutes; treat these as process references only and follow the selected product’s TDS for actual spread rate and open time.
3. Press and allow the bond to cure
Set pressure and press duration for the wood, joint profile, machine and adhesive. The source process gives 4–6 kg/cm² and 7–10 seconds as reference settings for vertical finger-joint equipment. Validate settings on the actual production line and allow adequate curing before machining or loading; do not apply these figures to every product or machine.
4. Clean tools and follow safety guidance
Clean adhesive containers and tools before and after work. If adhesive contacts skin, wash with soap and water. Refer to the product Safety Data Sheet (SDS) for current handling, storage and safety instructions.
TECHBOND technical support
TECHBOND can help manufacturers select an appropriate PVAc grade and review application conditions for their wood, joint design and equipment. See our industrial adhesive products or contact the TECHBOND team with your substrate, process and production requirements. Confirm product performance and operating parameters against current technical documentation before implementation. For independent background on PVAc, see the Encyclopaedia Britannica overview of polyvinyl acetate. Our technical team can also review samples and help manufacturers define a repeatable process window for each production line, including suitable adhesive viscosity, coating equipment, assembly time and pressing conditions.
TECHBOND Vietnam is a leading manufacturer of industrial adhesives in Vietnam. We specialize in providing a wide range of flexibly customized adhesive products to meet the diverse requirements of our customers.
Need advice on the right industrial adhesive?
Share your materials, application and production process. TECHBOND will help recommend a suitable solution.
Request a consultation